Custom Magnetic Chucks for EDM

Why Precision EDM Requires a Different Workholding Approach

EDM machining demands more than accurate positioning. Complex cavities, narrow cutting paths, and limited contact surfaces make conventional clamping difficult. For both wire EDM and sinker EDM, the fixture must keep the machining area accessible while maintaining stable workpiece positioning throughout the process.

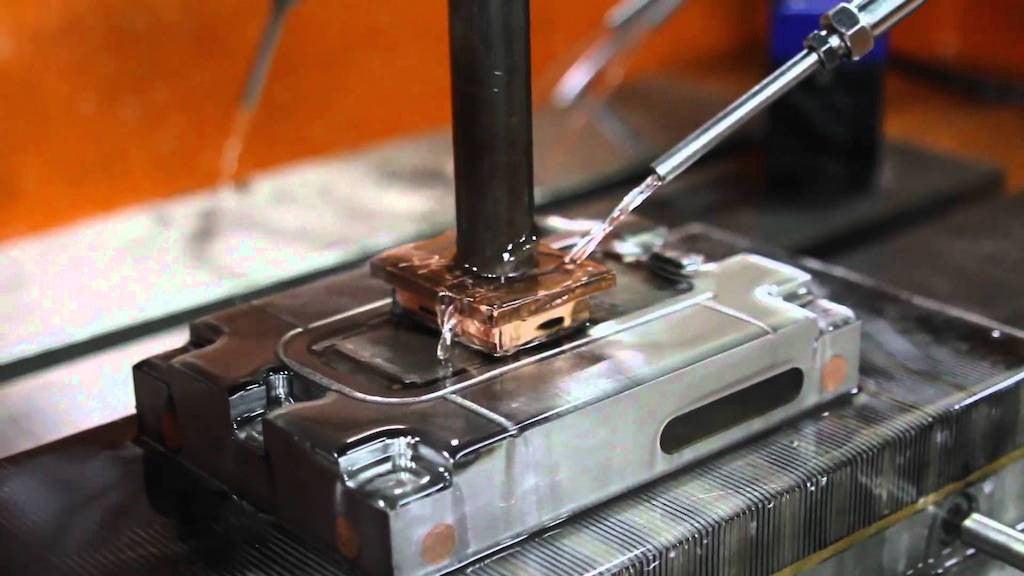
Copper electrode machining a steel workpiece in an EDM machine

Precision Holding Without Machining Interference

Traditional clamps can obstruct electrode movement, wire travel, or flushing access. Magnetic workholding offers a potential alternative for suitable steel components, helping reduce fixture interference while keeping critical machining areas accessible.

  • Unrestricted electrode and wire access
  • Stable positioning for precision components
  • Clearance for flushing and dielectric flow
  • Reliable contact on complex workpieces

Custom Magnetic Workholding Solutions for EDM Applications

No two EDM setups have exactly the same requirements. MAGWORK helps match magnetic chuck configurations to your workpiece geometry, machining method, and machine setup—providing practical solutions beyond standard chuck sizes and layouts.

01

Magnetic Contact & Workpiece Size

For small mold inserts or narrow steel components, fine-pole magnetic chucks can provide more effective pole engagement across limited contact areas, helping secure parts that are difficult to hold with conventional clamps.

02

Electrode & Wire Path Clearance

Custom magnetic pole layouts, support blocks, and fixture openings can be arranged around the machining zone, keeping electrode access, wire travel, and flushing paths clear.

03

Machine & Process Compatibility

Adapt chuck dimensions, mounting interfaces, and operating arrangements to suit wire EDM or sinker EDM machines, including dielectric exposure, positioning, and release requirements.

Discuss Your Workholding Requirements

Magnetic Workholding for Precision Mold & Die EDM

Small mold inserts, tool-steel components, and complex cavities often leave limited space for conventional clamps. For suitable ferromagnetic workpieces, magnetic holding can provide a more accessible setup for sinker EDM and wire EDM, particularly when machining intricate features or multiple surfaces.

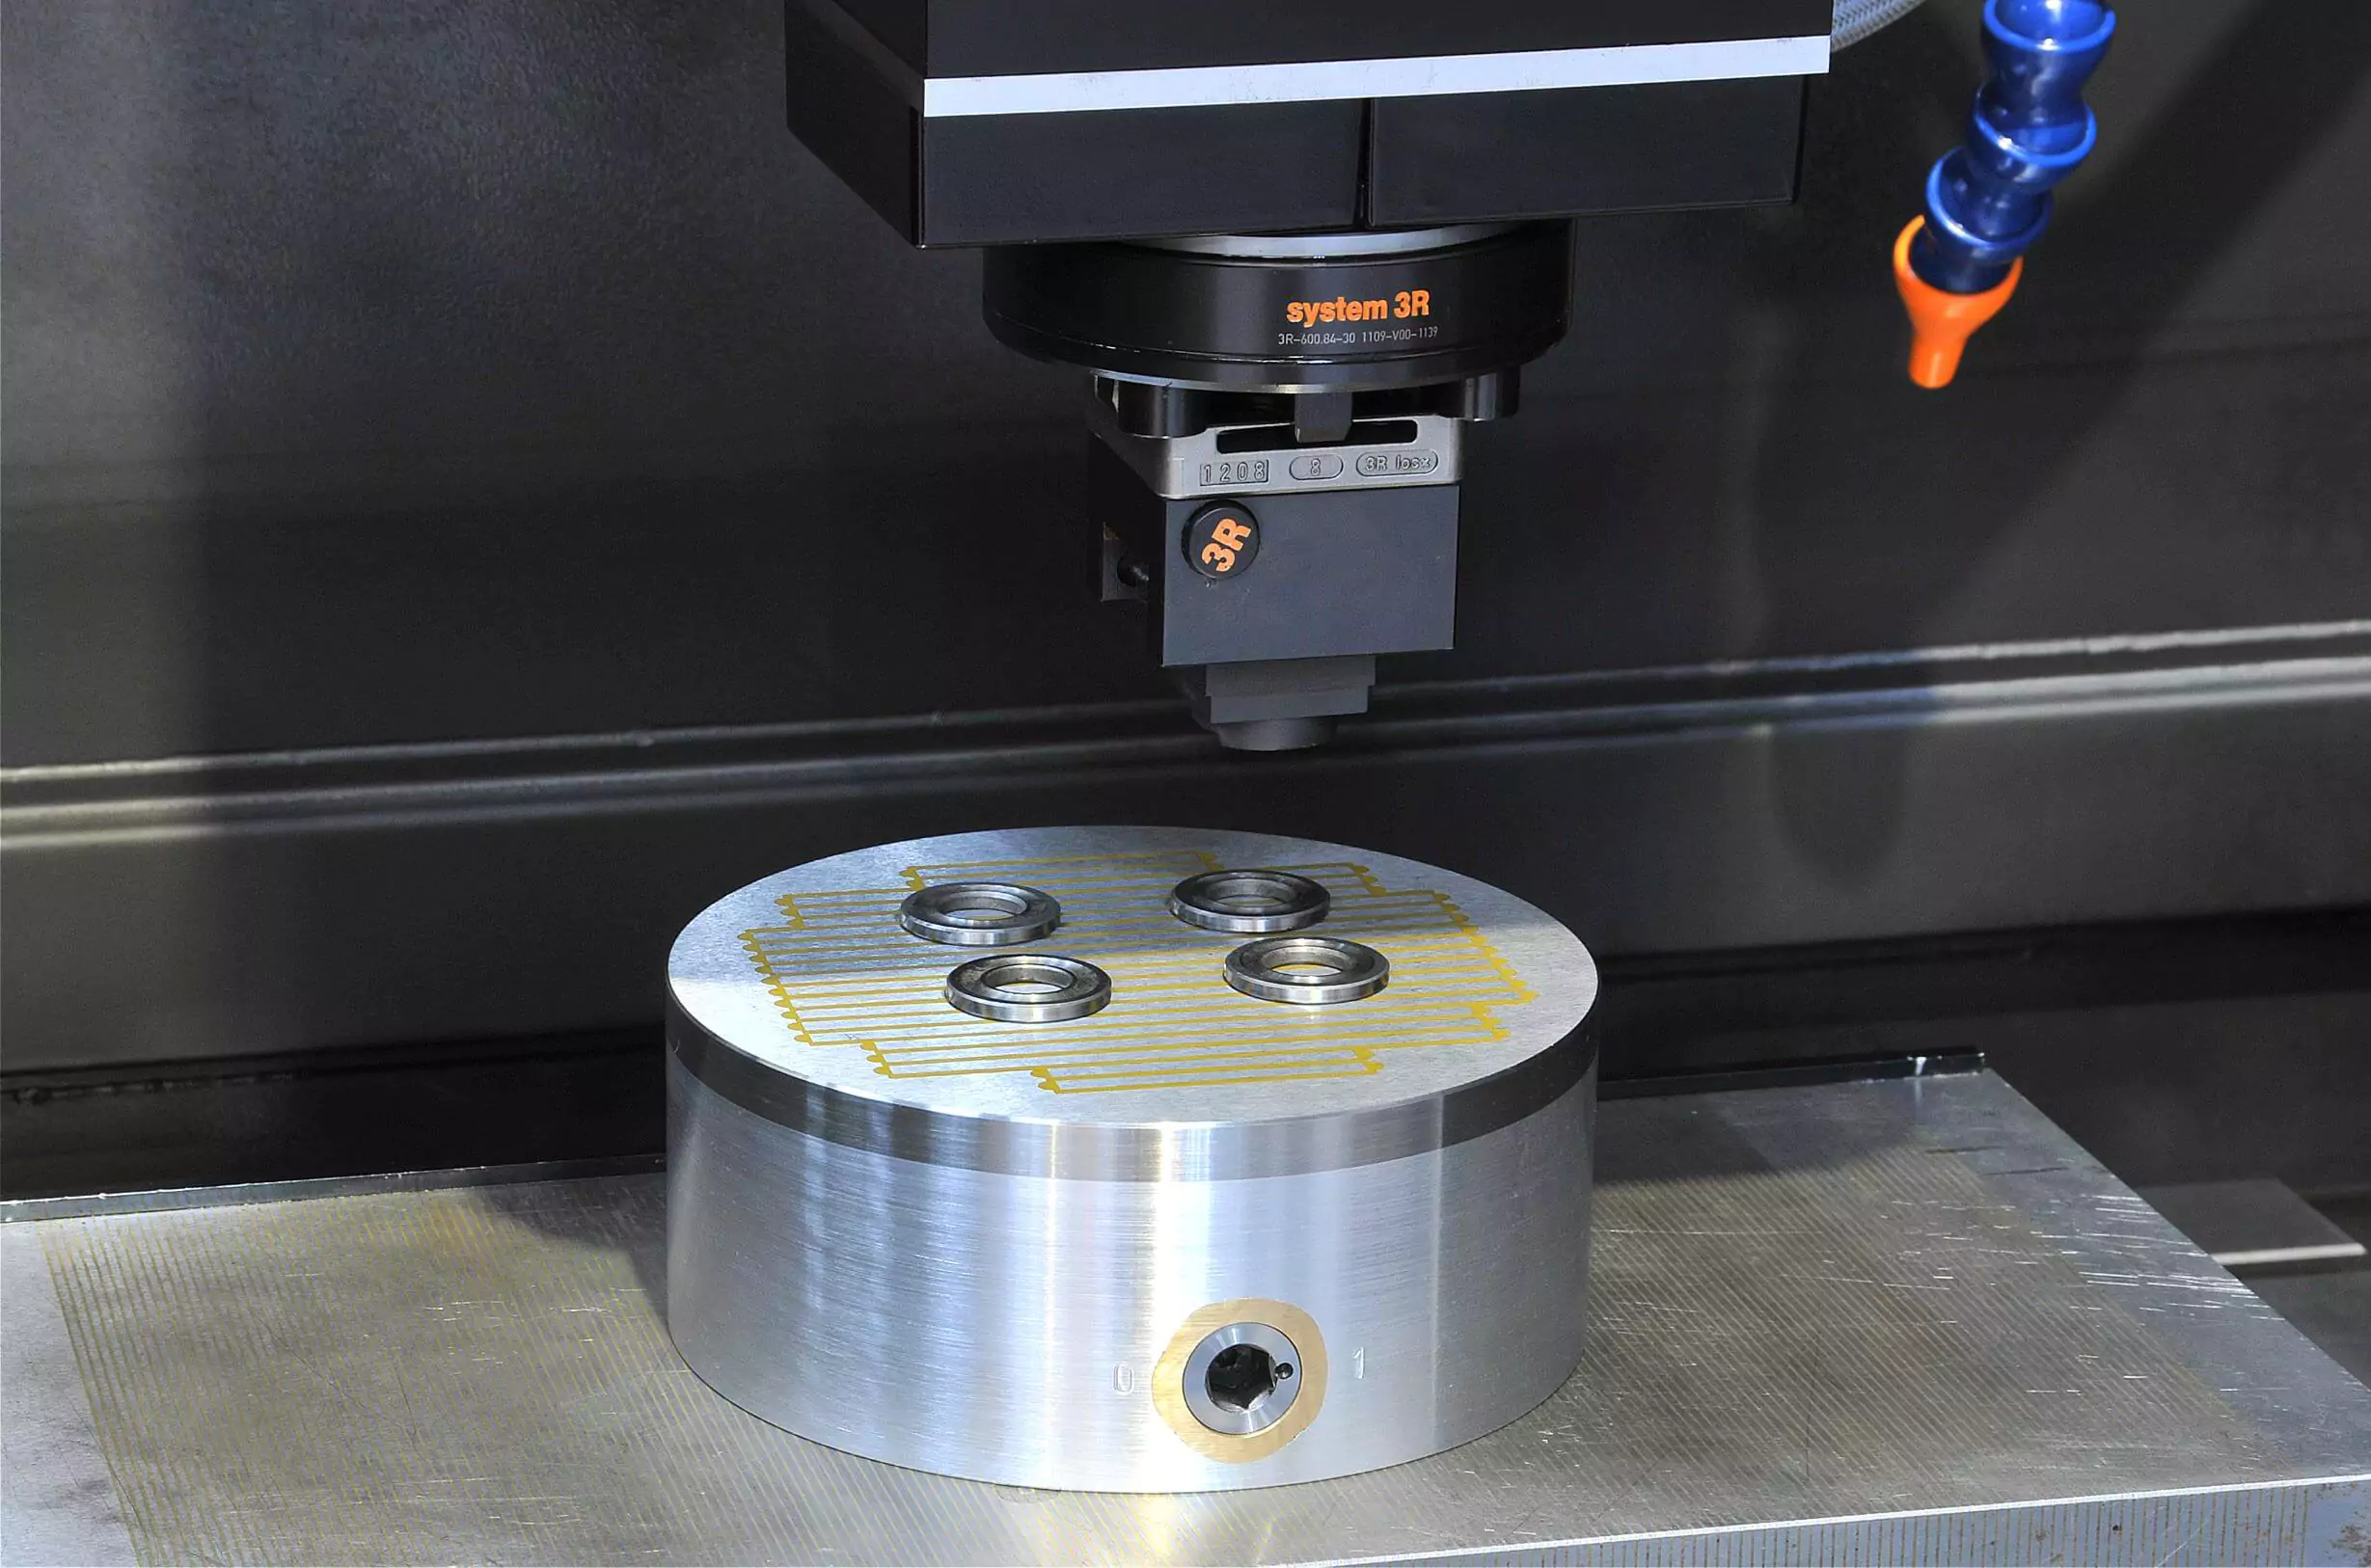
High precision round magnetic workholding chuck compatible with System 3R zero-point system for die sinking EDM

Less Clamping. More Freedom for Complex EDM Work.

When machining intricate mold cavities or small precision inserts, conventional clamps can get in the way. A custom EDM magnetic chuck can help free up valuable machining space, reduce repeated clamping adjustments, and keep suitable steel components securely positioned.

With the right magnetic pole arrangement and support design, even challenging workpiece geometries can benefit from a more accessible and practical EDM setup.

From Your EDM Requirements to a Custom Magnetic Chuck

A good EDM fixture starts with your machining needs—not a standard product size. MAGWORK coordinates custom magnetic chuck design and manufacturing, bringing together pole configurations, machine interfaces, and practical operating requirements to create a solution tailored to your application.

Engineered for Your EDM Process

From compact fine-pole magnetic chucks to custom mounting arrangements, we focus on the details that make your fixture practical to use. Each configuration is developed around your workpiece, EDM machine, and machining requirements.

Clearance

Electrode & wire access

Contact

Suitable magnetic pole layout

Mounting

Custom machine interfaces

Protection

Dielectric & corrosion resistance

Compact permanent magnetic chuck with a fine working face

Keep the Cutting Zone Clear for Wire EDM & Sinker EDM

A magnetic chuck should make EDM machining easier—not restrict where the electrode or wire can reach. MAGWORK considers machining paths, fixture height, flushing access, and operating conditions to help keep critical areas accessible and reduce unexpected setup interference.

ENGINEERING CHECK / 01

Sinker EDM — Electrode Clearance

Allow sufficient space for electrode travel, deep cavities, and flushing without interference from fixture components.

ENGINEERING CHECK / 02

Wire EDM — Cutting Path Access

Keep wire entry, cutting paths, lower guides, and slug removal areas clear throughout machining.

ENGINEERING CHECK / 03

Dielectric & Flushing Conditions

Consider dielectric exposure, flushing flow, and debris removal to support stable EDM operation.

ENGINEERING CHECK / 04

Fixture Height & Machine Travel

Check fixture height, workpiece position, and machine travel to avoid collisions and unnecessary setup restrictions.

Send Your Drawing for Selection Support
Copper electrode machining a steel workpiece in an EDM machine

Choosing the Right Magnetic Workholding for Different EDM Jobs

APPLICATION / 01

Die-Sinking EDM for Mold Components

Complex mold cavities require stable positioning without bulky clamps surrounding the machining area. Custom magnetic fixtures can help keep suitable steel mold components accessible while accommodating different cavity depths and workpiece sizes.

APPLICATION / 02

Wire EDM for Tool-Steel Plates

Wire-cutting often involves through-cuts and separated sections. A suitable magnetic fixture can support the remaining workpiece while dedicated relief areas and auxiliary supports accommodate the cutting process and cutout removal.

APPLICATION / 03

Small Precision Punches & Inserts

Small components may have too little contact area for conventional magnetic poles. Fine-pole magnetic chucks, combined with suitable locating features, can improve magnetic engagement and make repeated positioning more practical.

Make Sure Your Magnetic Chuck Works with Your EDM Machine

A magnetic chuck that fits your workpiece may not fit your EDM machine or operating environment. MAGWORK reviews mounting requirements, dielectric exposure, and operating conditions before production—helping you avoid compatibility issues, unnecessary modifications, and costly delays.

REVIEW 01 / 03

Machine & Installation Compatibility

Confirm mounting dimensions, table interfaces, fixture height, and machine clearances to ensure the magnetic chuck fits your EDM setup.

REVIEW 02 / 03

Dielectric & Corrosion Protection

Review fluid compatibility, sealing, corrosion-resistant materials, and electrical protection where applicable to support reliable operation in EDM environments.

REVIEW 03 / 03

Function & Acceptance Requirements

Define positioning accuracy, magnetic switching, release performance, and agreed inspection criteria before manufacturing to reduce unexpected issues during installation.

Which Magnetic Workholding Technology Fits Your EDM Process?

The best EDM magnetic chuck isn't necessarily the strongest or most expensive. MAGWORK helps you compare magnetic holding technologies based on operating convenience, workpiece requirements, and control needs—so you can choose a practical solution without unnecessary complexity.

01

Permanent Magnetic Chucks

Simple manual switching without continuous power. A practical choice for compatible EDM setups where straightforward operation and lower system complexity are priorities.

02

Electromagnetic Chucks

Electrically controlled magnetic holding, with adjustable force on suitable systems. Consider when variable holding control is useful and the machine supports the required electrical integration.

03

Electro-Permanent Magnetic Chucks

Electrical switching with no continuous holding current. Suitable for consideration when convenient activation and repeated workpiece loading are important, subject to EDM environment compatibility.

04

Magnetic Holding with Additional Support

For workpieces with limited contact areas or special positioning needs, custom magnetic chucks can be combined with locating stops and support blocks to improve stability and accommodate challenging EDM setups.

EDM Magnetic Chuck Quality Checks Before Delivery

A magnetic chuck that meets dimensional requirements may still create problems during EDM machining. MAGWORK coordinates inspections of critical dimensions, magnetic performance, and operating functions against agreed specifications—helping reduce installation issues, unexpected rework, and production delays.

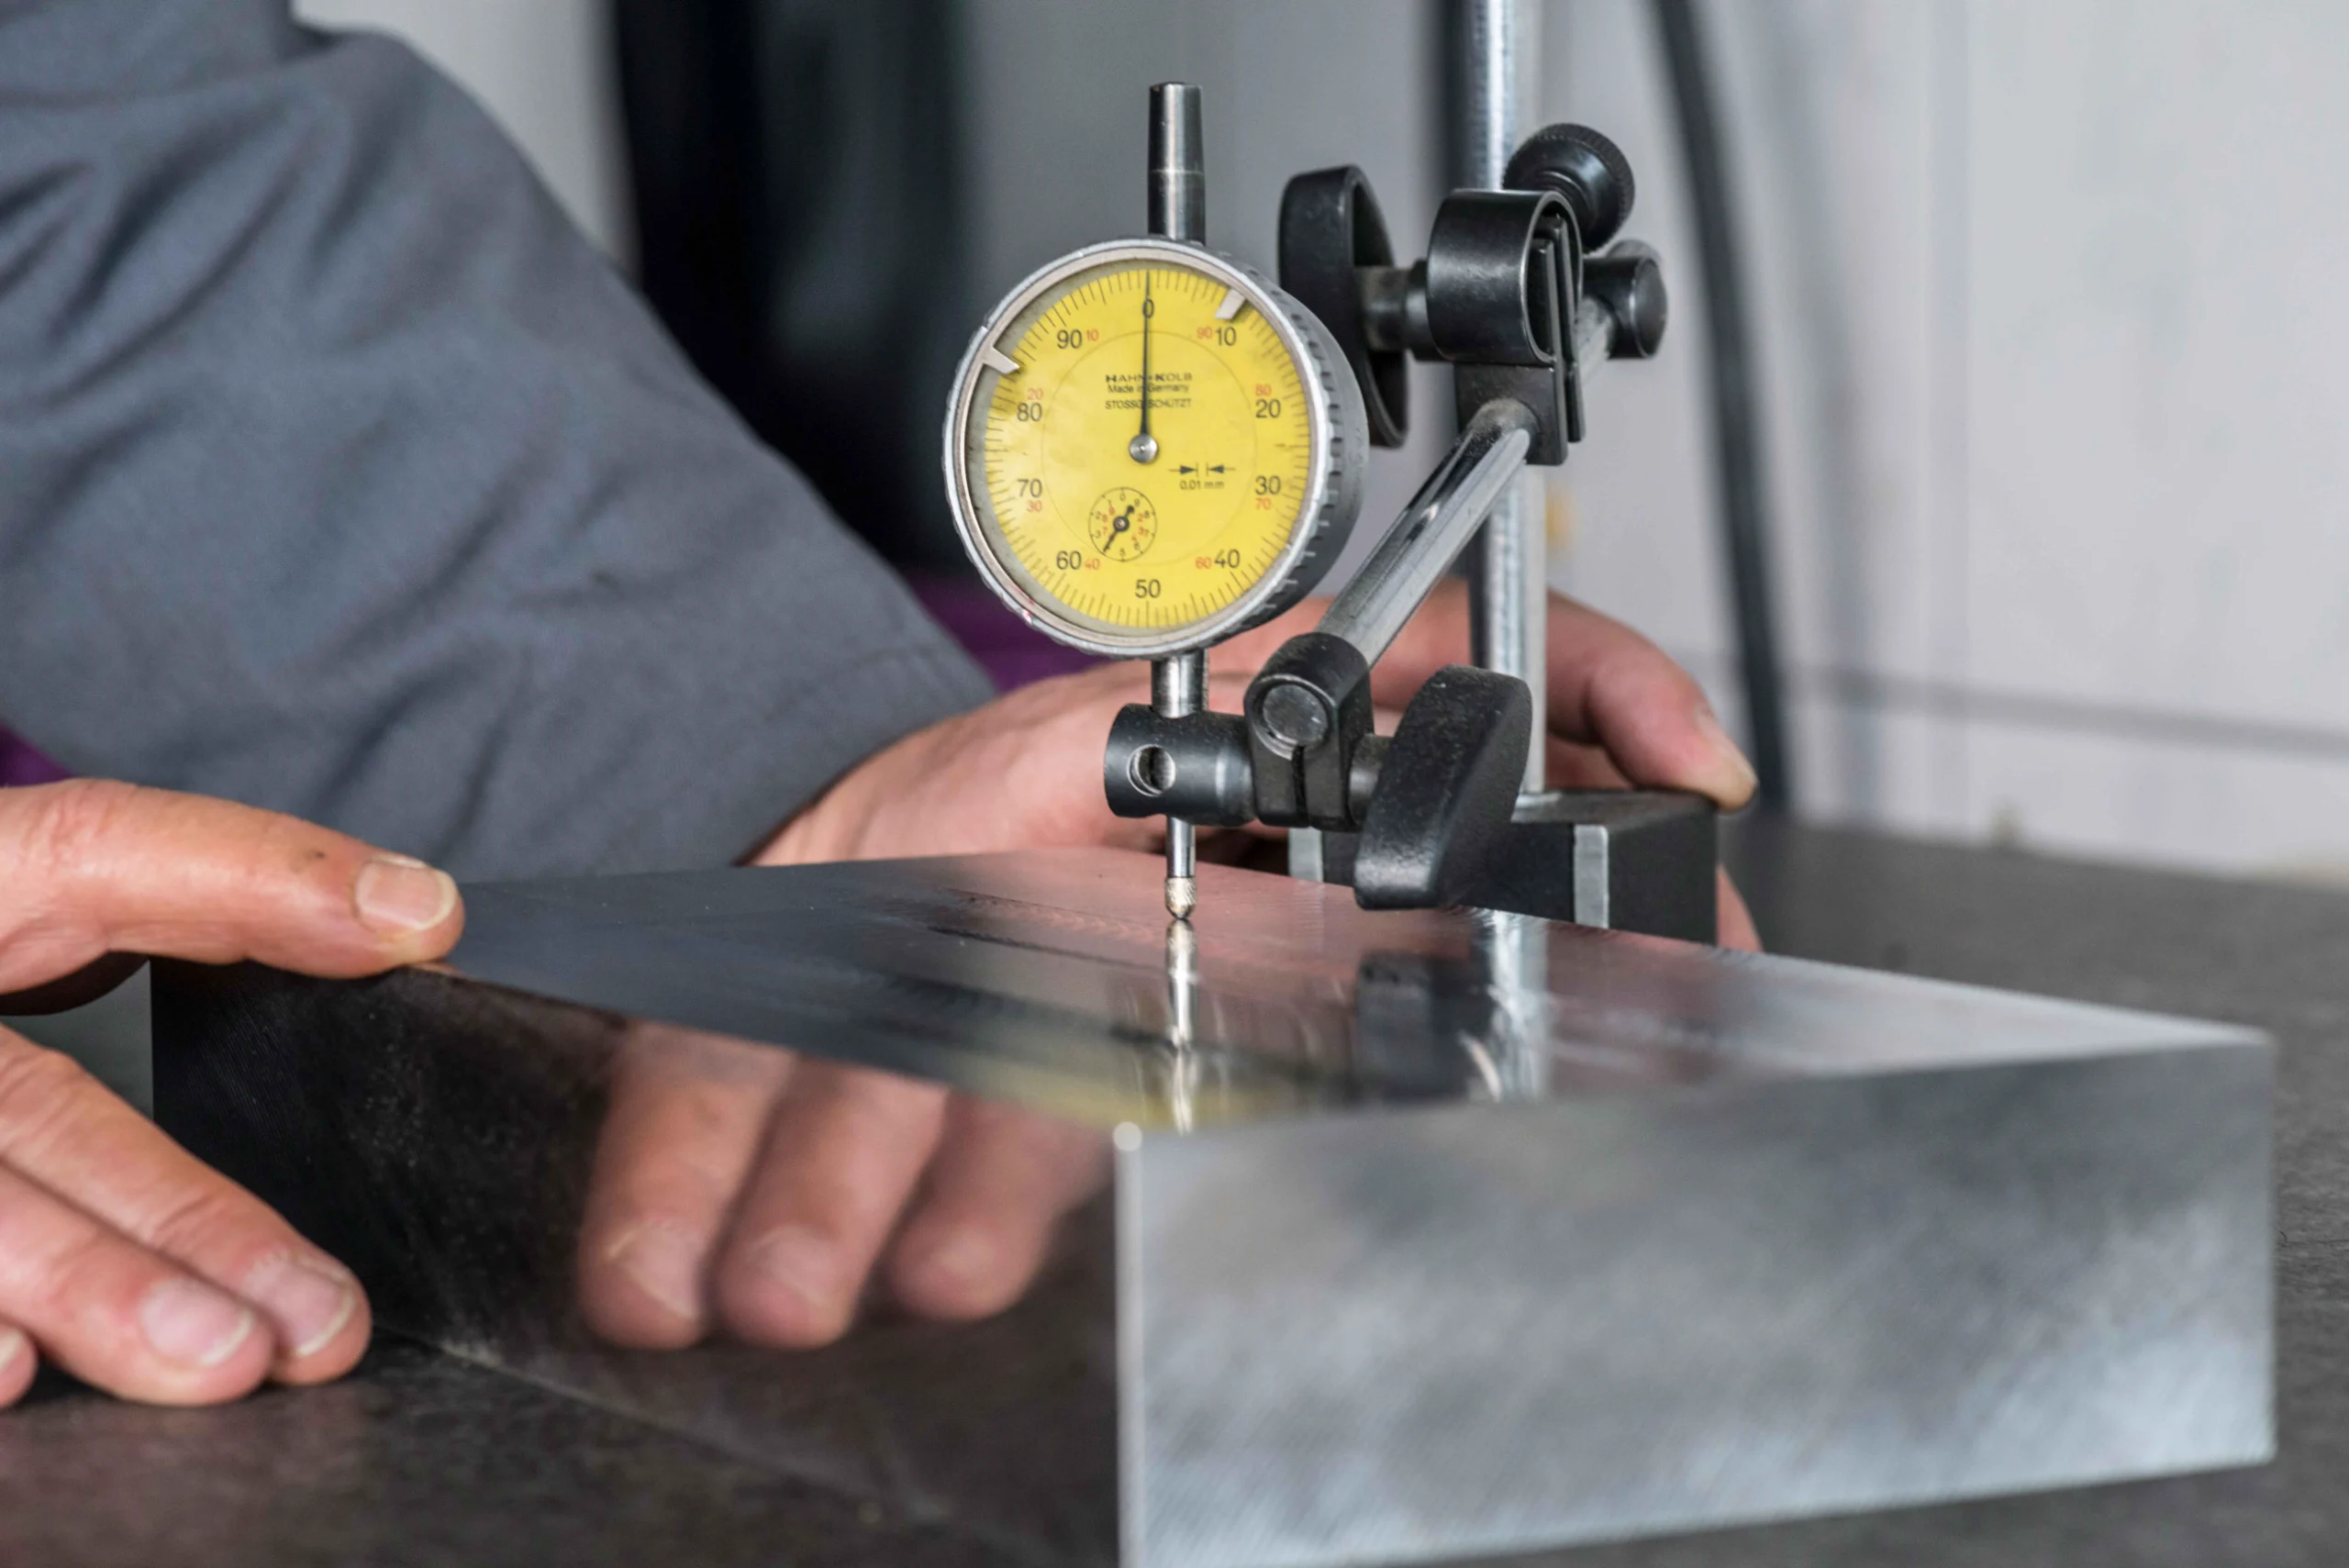
Dial caliper checking a magnetic chuck dimension
Verified for Your EDM Requirements

Quality goes beyond appearance. We focus on the details that affect how your magnetic chuck fits, holds, and operates, with inspection requirements tailored to the actual EDM application.

01 / QUALITY CHECK

Dimensional Accuracy

Working-face geometry, mounting dimensions, and critical interfaces.

02 / QUALITY CHECK

Magnetic Holding

Magnetic function and holding performance under agreed test conditions.

03 / QUALITY CHECK

Environmental Protection

Sealing, corrosion protection, and dielectric compatibility as specified.

04 / QUALITY CHECK

Switching & Release

Magnetic activation, workpiece release, and residual magnetism where applicable.

From Your EDM Requirements to a Ready-to-Use Magnetic Fixture

Custom EDM workholding shouldn't mean complicated sourcing or endless technical follow-ups. MAGWORK coordinates engineering communication, production progress, quality checks, and delivery through one point of contact—helping you save time and keep your EDM fixture project on track.

01Requirement Review

Share workpiece drawings, material, EDM process, and machine details.

02Technical Evaluation

Assess application feasibility and suitable magnetic workholding options.

03Fixture Proposal

Receive a recommended magnetic chuck configuration for your EDM application.

04Drawing Approval

Confirm fixture dimensions, mounting details, and agreed specifications.

05Material Preparation

Arrange materials and components for the approved design.

06Machining & Testing

Coordinate manufacturing, assembly, and agreed quality checks.

07Packing & Shipment

Protective packaging, export documentation, and delivery coordination.

08Technical Support

Assistance with installation, operation, and product-related questions.

EDM Magnetic Chuck & Custom Workholding FAQs

Find answers to common questions about EDM magnetic chucks, custom fixture design, workpiece compatibility, and magnetic workholding solutions for wire EDM and sinker EDM applications.

Can magnetic chucks be used for both wire EDM and sinker EDM?

Yes, magnetic workholding can be considered for suitable ferromagnetic components in both processes. However, wire EDM requires clearance for wire travel and cutout removal, while sinker EDM needs electrode access and suitable support around the machining area. Each setup requires application-specific evaluation.

Can MAGWORK design a custom magnetic chuck for my EDM machine?

Yes. MAGWORK can help develop custom EDM magnetic chucks with tailored dimensions, magnetic pole arrangements, locating features, and mounting interfaces based on your workpiece, machining process, and equipment requirements.

Can magnetic chucks hold small mold inserts and precision components?

For suitable steel components, fine-pole magnetic chucks can improve magnetic engagement across small contact surfaces. Actual holding performance depends on material properties, workpiece thickness, contact area, and the selected magnetic configuration.

Can magnetic workholding reduce clamping interference during EDM?

Yes, in suitable applications. Magnetic holding can reduce bulky mechanical clamps around the machining area, improving access for electrodes or wire paths. The fixture must still provide adequate support and positioning throughout machining.

Will EDM dielectric fluid affect magnetic chuck performance?

It depends on the chuck construction and operating environment. Sealing, corrosion protection, fluid compatibility, and electrical requirements must be reviewed. Not every magnetic chuck is suitable for immersion or continuous dielectric exposure.

Which magnetic chuck type is best for wire EDM?

There is no universal choice. Permanent, electromagnetic, and electro-permanent magnetic chucks offer different operating and control methods. The appropriate configuration depends on workpiece size, contact conditions, machine compatibility, and loading requirements.

Can magnetic workholding support repeated EDM production setups?

Suitable magnetic fixtures with defined locating features can simplify repeated workpiece positioning and loading. Actual repeatability depends on fixture accuracy, contact conditions, and the machining process.
Your EDM Process Deserves More Than a Standard Chuck

Complex mold cavities, small precision inserts, or restricted machining access? MAGWORK helps you explore custom EDM magnetic workholding solutions designed around your workpiece—not the limitations of standard fixtures.
Share your drawing or machining requirements. We'll help evaluate a practical magnetic chuck configuration for your application.