INDUSTRIES / AEROSPACE

Magnetic Workholding Solutions for Aerospace

Explore magnetic workholding for aerospace tooling production, focusing on suitable ferromagnetic parts such as steel fixture plates, hardened reference tools and ferrous drill jigs. MAGWORK supports drawing-based fixture discussion for real machining conditions, not claims of universal compatibility or completed industry projects.

Explore Application Concepts ↘
APPLICATION-LED ENGINEERING

Where Magnetic Chucks Fit Aerospace Manufacturing

Aerospace production tooling uses an assortment of workpieces, not a single magnetic-chuck standard. This page concentrates on ferromagnetic tooling and steel components where an open working face is valuable. Each example explains the machining task and the fixture decision that must be checked first.

We start with your drawings, grade, workpiece geometry, operation and machine. For suitable ferrous contact surfaces, an engineered magnetic fixture may help improve tool access. We assess whether support, locating stops and expected machining loads allow that approach before discussing a particular chuck technology.

Steel tooling components positioned on a square-pole magnetic chuck
Illustrative industrial image. No completed customer project or performance result is implied.
WORKPIECES & APPLICATION CONCEPTS

Aerospace Magnetic Workholding Applications

The following are application concepts for aerospace production tooling, not claims of completed customer projects. Compare the geometry and process of each part with your own drawing before asking for a configuration.

01 / TOOLING & DIE COMPONENTS

Milling aerospace steel tooling and die plates

Aircraft-related production fixtures may use steel tooling even when the finished aircraft part is nonmagnetic. Evaluate only the ferromagnetic tooling surface, not the aircraft part itself.

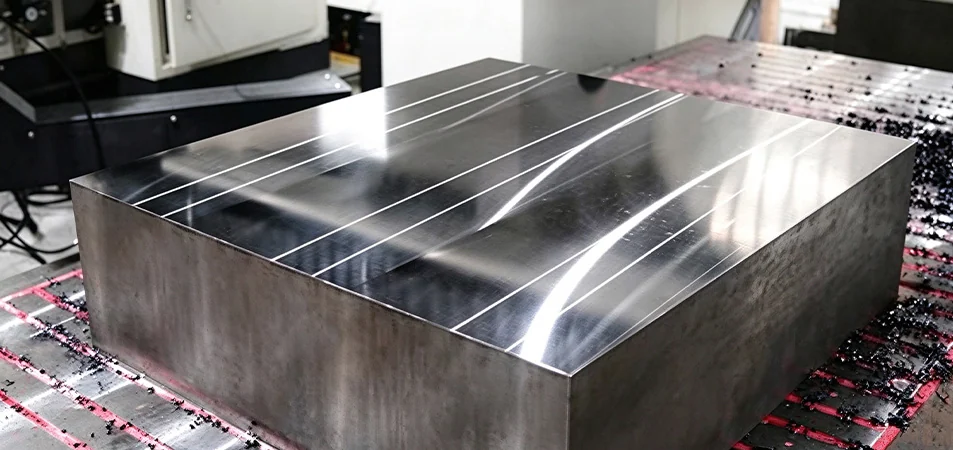
Steel block with its upper machining face clear of top clampsShaped metal component on a round magnetic fixture

Machining space without losing positive location

Define accessible milling faces, stable reference edges and approved fixture mounting before selecting the magnetic system.

For this aerospace tooling production concept, the final drawing should identify usable magnetic contact, locating references and any nonmagnetic zones. Engineering checks: Milling forces, locating stops, underside contact and surface protection. The proposal should state the fixture limits, proposed inspection scope and any conditions that require a mechanical alternative. Check the proposed fixture against the actual workpiece and cutting conditions before production.

WORKPIECESTool-steel plates, die components and hardened steel inserts
FIXTURE CONCEPTMagnetic holding face with tailored locating stops and local supports
CHECK FIRSTMaterial, contact footprint, machining force, cutter access and relief areas
VERIFYPosition repeatability, finished dimensions and holding conditions
02 / DRILL JIGS & TOOL PLATES

Drilling ferrous drill-jig plates

A ferrous drill template may have tight hole-to-hole spacing. Clearance around each breakthrough point is essential to protect the magnetic face.

Machining a hole pattern in steel workpieces on magnetic chucksSteel tooling components positioned on a square-pole magnetic chuck

Design around the entire hole pattern

Locate magnetic contact outside exit paths and keep hard stops accessible to the operator.

For this aerospace tooling production concept, the final drawing should identify usable magnetic contact, locating references and any nonmagnetic zones. Engineering checks: Breakthrough clearance, hole spacing, drill thrust and fixture mounting. The proposal should state the fixture limits, proposed inspection scope and any conditions that require a mechanical alternative. Check the proposed fixture against the actual workpiece and cutting conditions before production.

WORKPIECESFerrous tooling plates and production fixture bases
DESIGN FOCUSHole access, repeat loading and support under drilling locations
CHECK FIRSTDrill thrust, through-hole clearance, chip path and stop position
VERIFYSetup repeatability and agreed workpiece inspection criteria
03 / PRECISION GROUND FIXTURES

Grinding hardened steel reference tooling

Hardened gauge and reference tooling demands predictable positioning during finishing. The contact surface needs to be free of chips and burrs.

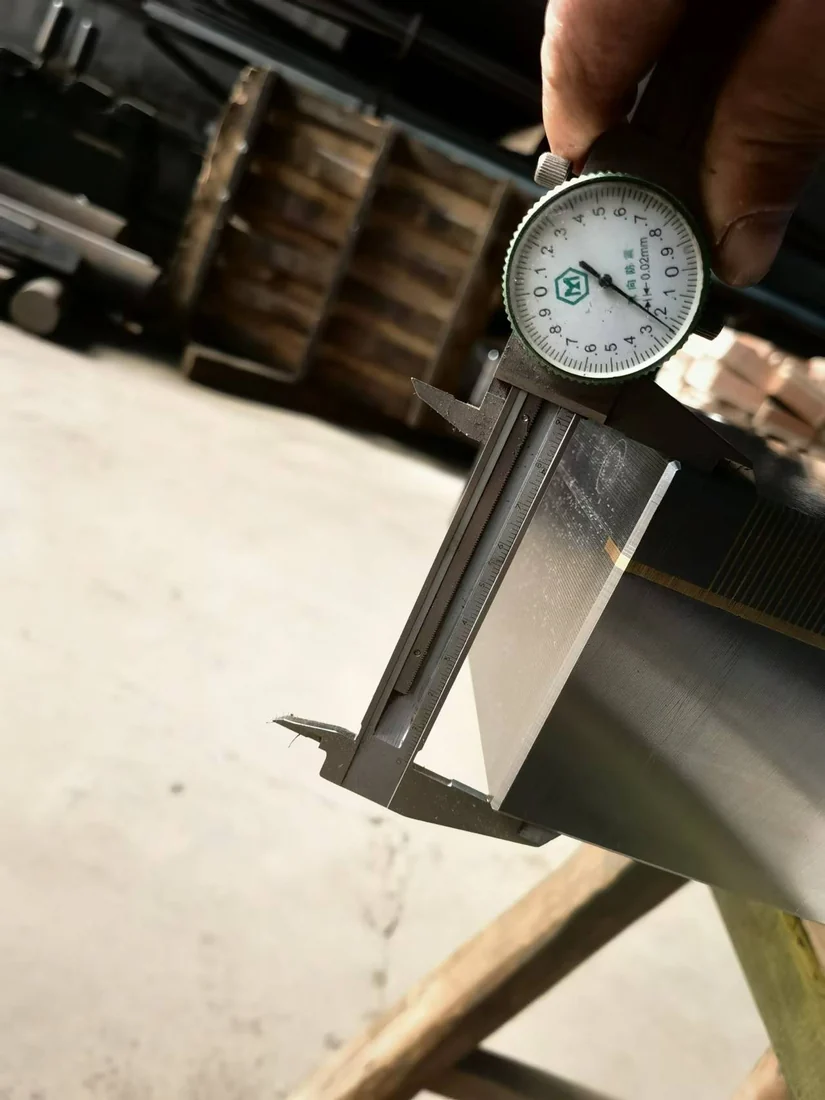
Surface grinding a flat steel workpieceDial caliper checking a magnetic chuck dimension

Fit the pole layout to the fixture geometry

Prioritize face finish, datum repeatability and a documented measurement method, without promising an unverified aerospace certification.

For this aerospace tooling production concept, the final drawing should identify usable magnetic contact, locating references and any nonmagnetic zones. Engineering checks: Thickness, pole spacing, finish requirements and release behavior. The proposal should state the fixture limits, proposed inspection scope and any conditions that require a mechanical alternative. Check the proposed fixture against the actual workpiece and cutting conditions before production.

WORKPIECESFlat ferrous components, tool inserts and steel plates
DESIGN FOCUSSupport distribution and appropriate magnetic pole layout
CHECK FIRSTThickness, magnetic material properties and ground area
VERIFYFlatness, surface condition and demagnetization where needed
CUSTOM MAGNETIC FIXTURE ENGINEERING

Custom Magnetic Fixture Engineering for Aerospace

For aerospace production tooling, a custom magnetic fixture starts with a specific contact face and machine interface. Pole layout, support blocks, stop locations and clearance should be chosen from the actual part geometry. Standard chuck dimensions are only a starting reference.

Confirm material response before specifying magnetic holding. In ferrous production tooling and traceable setup, the relevant workpiece is a ferromagnetic tooling component; nonmagnetic finished parts may instead require a dedicated adapter or conventional mechanical fixture.

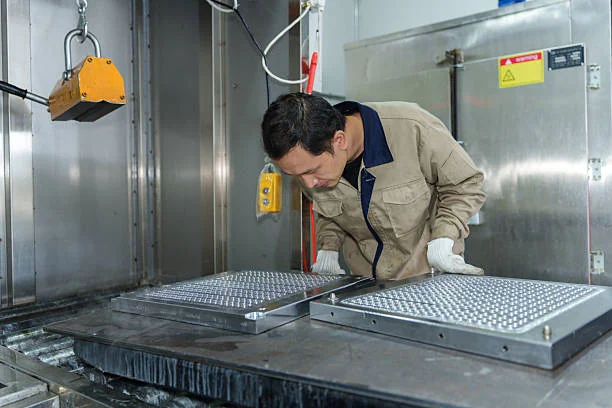
Workshop floor with machine tools and prepared magnetic chuck components
ENGINEERING & PRODUCTION CAPABILITY

Magnetic Chuck Manufacturing and Testing Capability for Aerospace

The manufacturing gallery shows general workholding production stages: machined bodies, pole components, assembly, finishing and inspection. For a aerospace production tooling order, the agreed mounting dimensions and acceptance points determine what must be checked on the finished chuck.

01 / 06 · ENGINEERING DESIGN

Designed around the workpiece

For tooling bases and drill templates, the engineering review connects magnetic pole placement to the actual machining and machine mounting. Reference edges, stops and support zones should be visible on the approved fixture drawing.

Workpiece reviewContact & pole layoutDesign confirmation

Production images illustrate body machining, assembly, finishing and inspection. Confirm any industry-specific process or performance claim against records for the supplied fixture.

PROJECT SUPPORT / AEROSPACE

Engineering and After-Sales Support for Aerospace Fixtures

Technical support for aerospace production tooling projects concentrates on drawing coordination, installation interfaces and practical operating guidance. Project documents should identify the selected chuck configuration, machine mounting, operating controls if applicable, and agreed checks before shipment.

01

Application & feasibility review

Before support can recommend a fixture for drill templates and hardened checking tools, confirm material and usable contact face. Identify the machining load direction and any installation restriction that may affect the proposed setup.

02

Drawing & configuration coordination

Technical coordination focuses on tooling base datums and controlled contact. Electrical controls are considered only when the selected magnetic technology uses a controller.

03

Inspection & delivery documents

Agree on acceptance evidence relevant to precision reference planes and repeatable mountings, including the dimensions and functional tests that the actual fixture needs, rather than a generic test checklist.

04

Setup & after-sales communication

After delivery, installation support should address approved fixture handling and dimensional inspection; maintenance advice must follow the supplied magnetic system and its operating method.

Operator checking magnetic chuck plates on a machine tableENGINEERING REVIEW → PRODUCTION → TECHNICAL SUPPORT
AEROSPACE / FAQ

Aerospace Magnetic Workholding FAQs

These answers clarify material suitability, application limits and what to confirm when evaluating a magnetic fixture for aerospace production tooling.

Can magnetic workholding hold titanium aerospace parts?

Titanium is not normally ferromagnetic, so a standard magnetic chuck cannot directly hold typical titanium aerospace parts. Evaluate mechanical fixtures or a suitable ferrous intermediary where appropriate. In aerospace tooling production, confirm the steel grade, real contact face and fixture clearance from the actual drawing. Do not present an illustrative application as a proven customer result.

What aerospace parts are the best starting point?

Selected steel tooling plates, die inserts, fixtures and hardened ferrous reference parts are more realistic candidates than most lightweight structural airframe parts. In aerospace tooling production, confirm the steel grade, real contact face and fixture clearance from the actual drawing. Do not present an illustrative application as a proven customer result.

How can fixture repeatability be checked?

Agree reference faces, loading sequence, stops, setup conditions and dimensional checks before approving the fixture. In aerospace tooling production, confirm the steel grade, real contact face and fixture clearance from the actual drawing. Do not present an illustrative application as a proven customer result.

Can through-holes be drilled on a magnetic chuck?

Only when the design provides drill clearance, sufficient support and protection for the magnetic working face. In aerospace tooling production, confirm the steel grade, real contact face and fixture clearance from the actual drawing. Do not present an illustrative application as a proven customer result.

What information is required?

Provide material grade, drawing, surface requirements, machine interfaces, machining loads and inspection criteria. In aerospace tooling production, confirm the steel grade, real contact face and fixture clearance from the actual drawing. Do not present an illustrative application as a proven customer result.
AEROSPACE / TECHNICAL INQUIRY

Request a Custom Magnetic Fixture for Aerospace

For a aerospace production tooling workholding review, provide the workpiece drawing and identify the machining face that must stay accessible. Add the machine model and material grade so the proposed fixture can be evaluated against a real task.

Request an application review

For the initial review, identify the representative workpiece and tooling base datums and controlled contact. Attach its drawing and machine interface details.

The project examples above are illustrative, not verified customer case studies. Replace reference photos and details with approved material before publishing.